About Carbon Black Cobalt Oxide
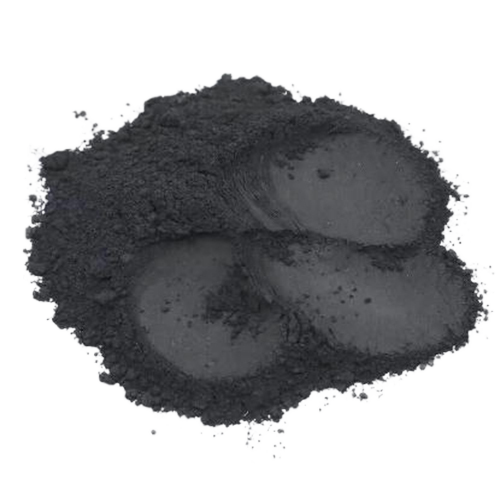
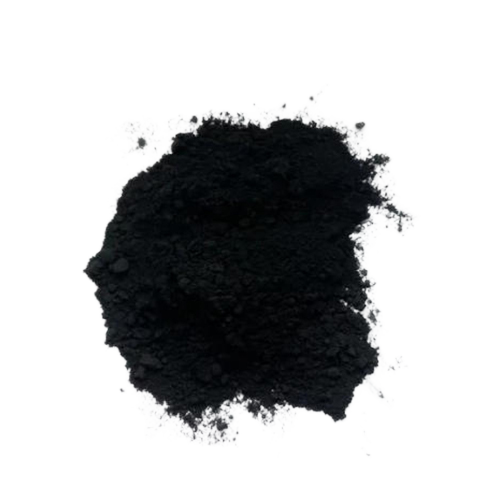
Capitalise on the peerless quality of Carbon Black Cobalt Oxide-engineered for monumental performance in industrial and technical applications. With a sizzling purity of 99% and a terrific molecular weight of 90.06 g/mol, this product sets the standard for versatility and efficacy. Its insolubility in water, high stability, and micron/submicron particle size ensure outstanding functionality. Try Now to experience the brilliance in pigments, battery materials, catalysts, or electronic applications. Available in HDPE bags (25 kg), it is non-hazardous, long-lasting, and ready for global shipment from China. Procure from a distinguished exporter, manufacturer, and supplier today.
Monumental Applications and Competitive Advantages
Carbon Black Cobalt Oxide finds widespread use in pigments, battery materials, electronic devices, and catalysts, delivering peerless performance. Its robust physical characteristics, including a high melting point and terrific stability, make it a superior choice for technical and industrial-grade projects. Other applications include coatings, ceramics, and magnetic materials. Competitive advantages feature prolonged shelf life, secure storage, and technical-grade purity, ensuring consistency and reliability in diverse settings.
Premium Packaging, Certainty in Shipment, and Samples Available
All Carbon Black Cobalt Oxide shipments are carefully packaged in secure 25 kg HDPE bags to maintain product integrity during transit and storage. Promptly dispatched upon order confirmation, this product is supported by certifications guaranteeing industrial-grade standards. Samples are available on request for evaluation and testing purposes, allowing customers to verify suitability before full-scale procurement. Experience worry-free, certified packaging tailored for international and domestic shipment needs.
FAQ's of Carbon Black Cobalt Oxide:
Q: How is Carbon Black Cobalt Oxide best stored to maintain its quality?
A: For optimal preservation, Carbon Black Cobalt Oxide should be stored in a cool, dry place, away from moisture and extreme temperatures, to uphold its 24-month shelf life.
Q: What primary industries benefit from using Carbon Black Cobalt Oxide?
A: Industries engaged in pigments, battery manufacturing, catalyst production, and electronic applications most benefit from its advanced chemical and physical properties.
Q: When can I expect shipment after confirming my order?
A: Shipment is typically dispatched promptly after order confirmation, depending on logistics arrangements. Packaging in 25 kg HDPE bags ensures product safety during transit.
Q: Where does Carbon Black Cobalt Oxide originate from and who supplies it?
A: This material is manufactured and exported from China by a leading supplier with extensive experience in industrial-grade inorganic compounds.
Q: What are the competitive advantages of using Carbon Black Cobalt Oxide in electronic applications?
A: The product's high purity, uniform particle size, and excellent stability confer substantial performance and reliability advantages in electronic and electrical applications.
Q: How can I obtain a sample before purchasing bulk quantities?
A: Samples are available on request. Contact your supplier to receive a sample for evaluation to ensure the product meets your specific requirements.




 Send Inquiry


 Send Inquiry
